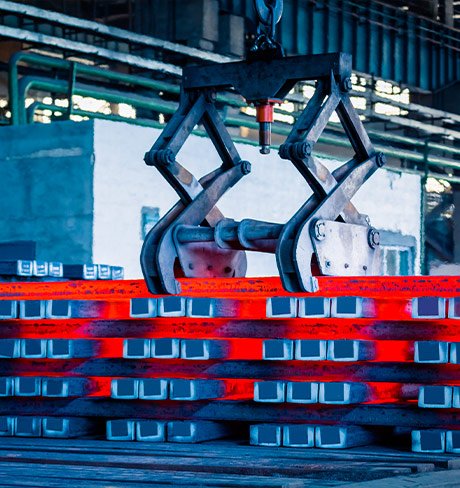
Our integrated manufacturing process extends from the manufacturing of direct reduced iron, commonly known as sponge iron, to the manufacturing of MS billets and their further conversion into finished steel products including, TMT bars, HR coils, CR coils, HR (MS) pipes, CR pipes and galvanized tubes and pipes. The Sponge iron, MS billets, HR coils and CR coils produced by us are primarily intended to be used for captive consumption in downstream manufacturing process; thereby supporting our integrated operations. Any production in excess of our captive requirements is sold in the open market. We also manufacture industrial products used in steel manufacturing, including met coke and ferro alloys such as silicon manganese and ferro silicon, which are sold in open market.
Our backward-integrated manufacturing operations enable us to exercise greater control over the availability and quality of intermediate products required for our downstream manufacturing processes and reduce our dependence on third-party suppliers. Our manufacturing processes also provide us with the flexibility to manufacture steel products across a range of formats, including various grades of TMT bars, specialized steel and alloy products, and tubes and pipes for varied applications.
Product wise manufacturing process:
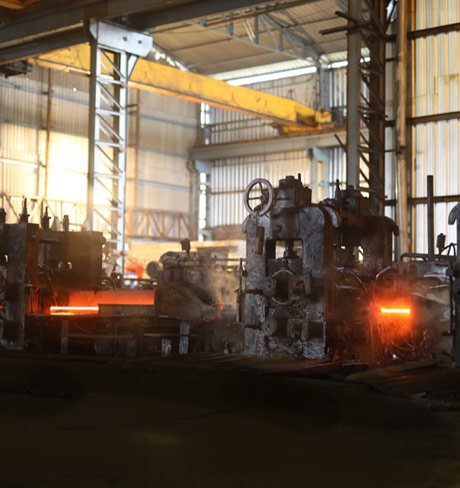
Here's our manufacturing process and technology in use
Our manufacturing operations span six facilities across Karnataka and Andhra Pradesh, covering multiple stages from raw material preparation and iron making to steel making, continuous casting, rolling and finishing. As of March 31, 2026, our aggregate installed capacity across intermediate, finished steel and industrial products was 17,33,100 MTPA.
Raw materials
Our manufacturing process uses key raw materials including scrap, iron ore, pellets, coal, coking coal, pig iron, wood charcoal, quartz and power. These materials are sourced through domestic and international market purchases, e-auctions, open-market operations and long-term supply arrangements.
In Fiscal 2026, raw materials accounted for 84.49% of our total expenditure.
Key features:
Multiple domestic and international sourcing channels
Long-term supply and linkage arrangements
Strategic locations close to major iron ore sources
Manufacturing facilities within approximately 450 km of major ports
Backward integration across several stages of production
Sponge iron
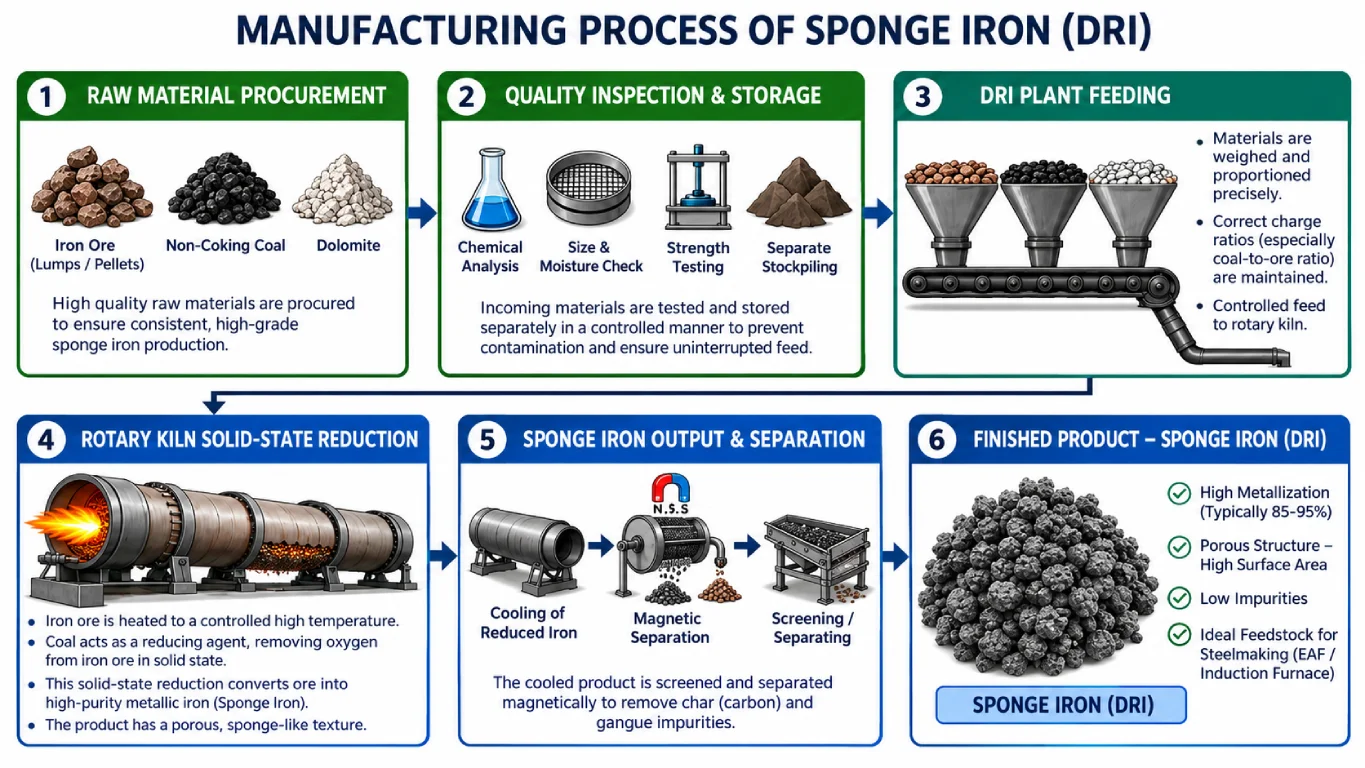
Sponge Iron, also known as Direct Reduced Iron (DRI), is an intermediate product with high iron content and is primarily used as a raw material for producing steel billets and other steel products.
We manufacture sponge iron at our Bellary Facility I and Koppal Facility.
FY2026 installed capacity: 2,50,000 MTPA
FY2026 production: 2,52,686 MT
Key features:
High iron content
Intermediate raw material for steelmaking
Supports our backward-integrated manufacturing process
Produced at two manufacturing facilities
Blooms – for high & fine quality steel bars
The fine raw material is processed to form Blooms, the source of high-quality TMT
Bars. 12 m 160×160 sq.cm., is used only by primary steel manufacturers. This results in better quality steel compared to secondary manufacturers using 6 m billet of 100×100 sq.cm
While the average billet size is 16 sq. inches and weighs 500 kg, A-One Gold Blooms are of 40 sq. inches size and weighs 2,500 kg.
Bloom makes better steel than billets because:
Bloom is 5 times heavier than Billet.
Bloom is 500% more consistent.
Bloom has a better grain structure.
Slower heat loss of Blooms ensures higher uniform quality across the bar.
MS Billets
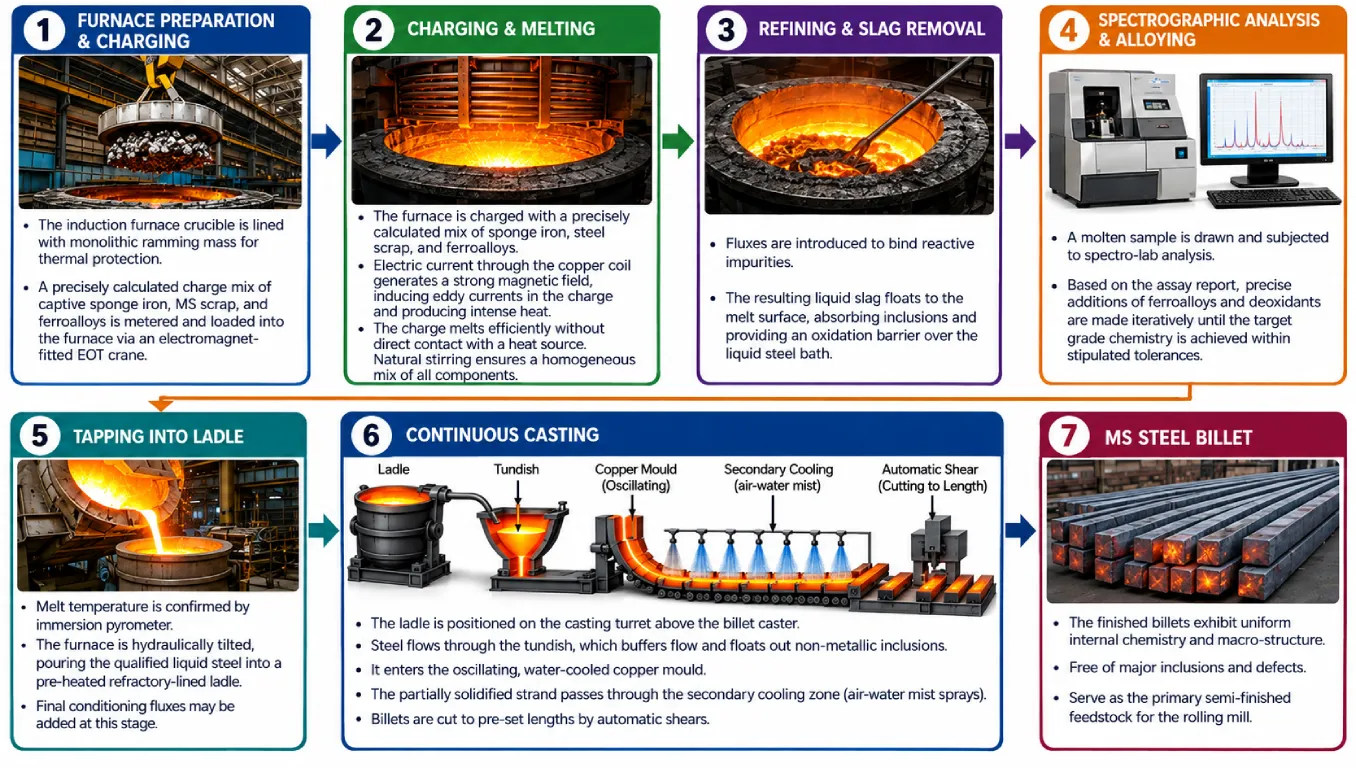
MS Billets are semi-finished steel products produced through the steelmaking and continuous casting process. Sponge iron, scrap and ferroalloys are charged into induction furnaces, where they are melted and refined. The molten steel is analysed and alloyed to achieve the required chemistry before being continuously cast into billets.
Our MS Billets are manufactured at Bellary Facility I, Gauribidanur and Hindupur.
FY2026 installed capacity: 5,70,000 MTPA
FY2026 production: 4,92,846 MT
Key features:
Controlled chemical composition
Continuous casting process
Used as feedstock for downstream rolling
Manufactured across three facilities
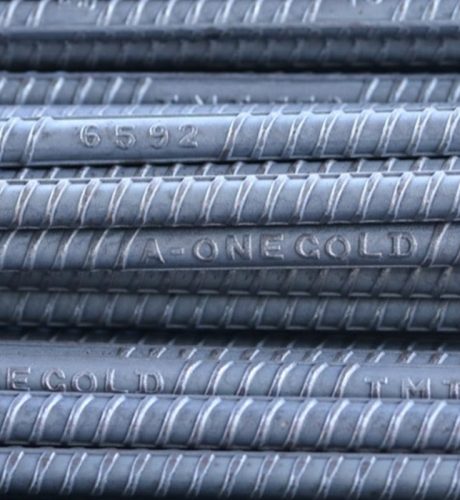
TMT Bars
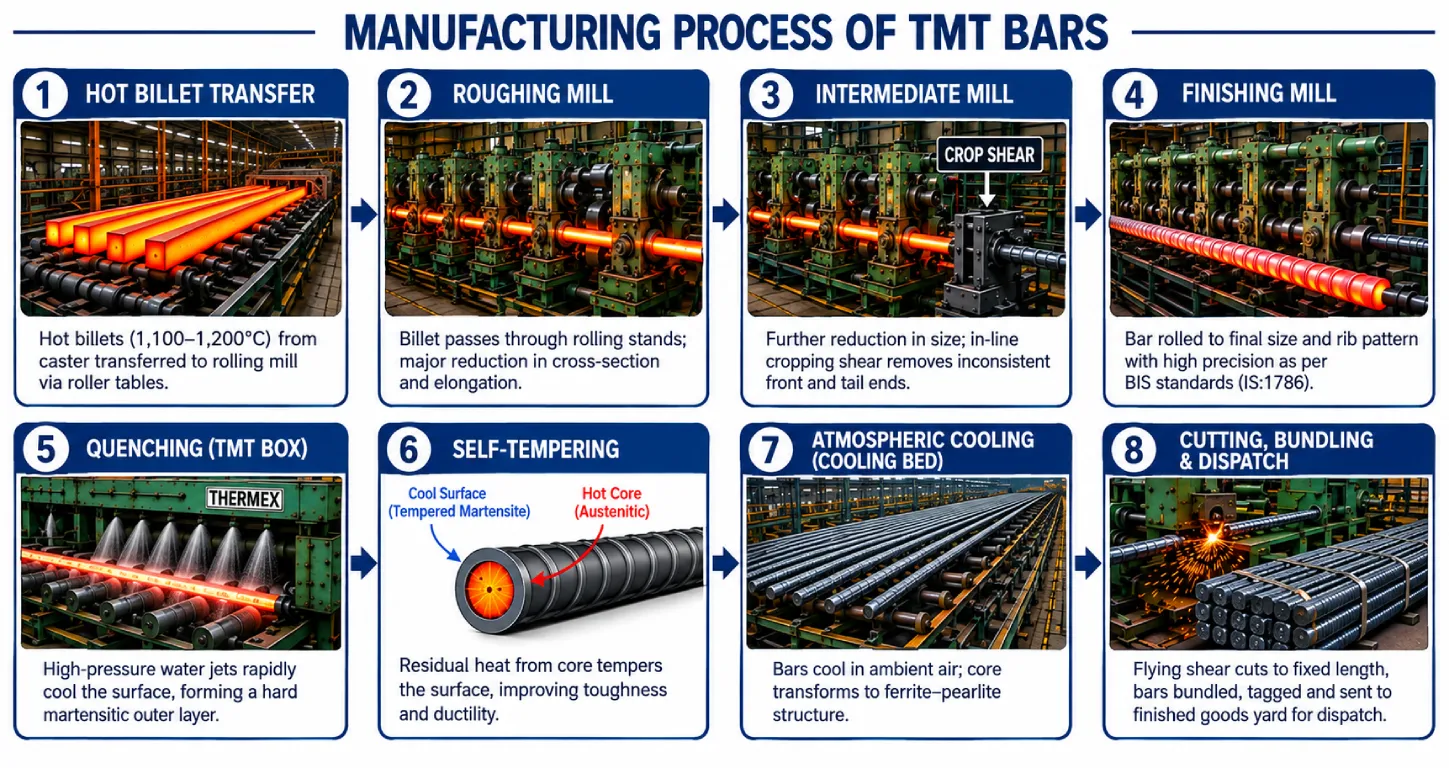
Our MS billets are converted into TMT reinforcement bars through automated rolling operations. Hot billets are transferred to the rolling mill, passed through successive rolling stands and then subjected to controlled quenching and self-tempering before cooling, cutting and inspection.
TMT Bars are manufactured at Gauribidanur and Hindupur.
Size range: 8 mm – 32 mm
FY2026 installed capacity: 3,36,000 MTPA
FY2026 production: 2,53,343 MT
Key features:
Thermo-mechanically treated
High strength and flexibility
Controlled rolling and quenching process
Used for reinforcement in construction and infrastructure
Latest Thermex (QST) Technology
German Technology – German Rolling Mill
The quenching and self-tempering process make use of the heat energy of the rolled bars. Usually, this energy is wasted as the rolled bars at 950-1000ºc are allowed to cool at ambient temperature on the cooling bed.
The bar, as it leaves the last stand guided through specially designed proprietary Thermex Pipes, wherein the surface temperature of 950-1000ºc is brought down drastically in a relatively short period, approximately in 1 second on account of the core being largely unaffected.
The drastic and pre-determined cooling of the bar’s edge transforms the peripheral structure to Martensite and would necessarily need to toughen up to render the bars beneficial. It is accomplished through the heat available at the core. The difference in the peripheral and the core temperature is finally equalized at around 600ºc and the resultant bar structure is of tempered martensite at Periphery and fine-grained Ferrite-Pearlite at the core.
The resultant soft-core forms about 65 – 75% of the area (depending upon the desired minimum yield strength), and the rest is the hardened edge. The product exhibits high yield points, surface hardness, toughness, ductility, and weldability.
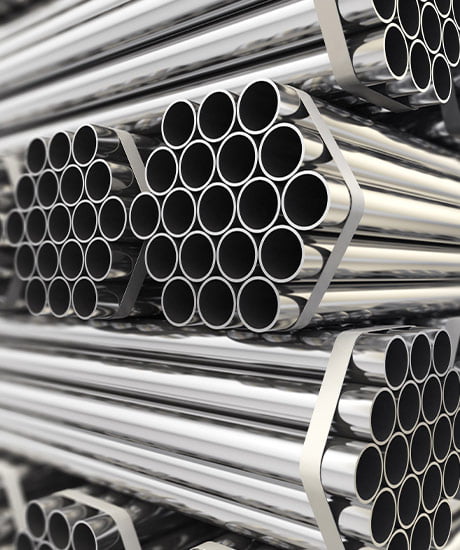
Pipes and tubes
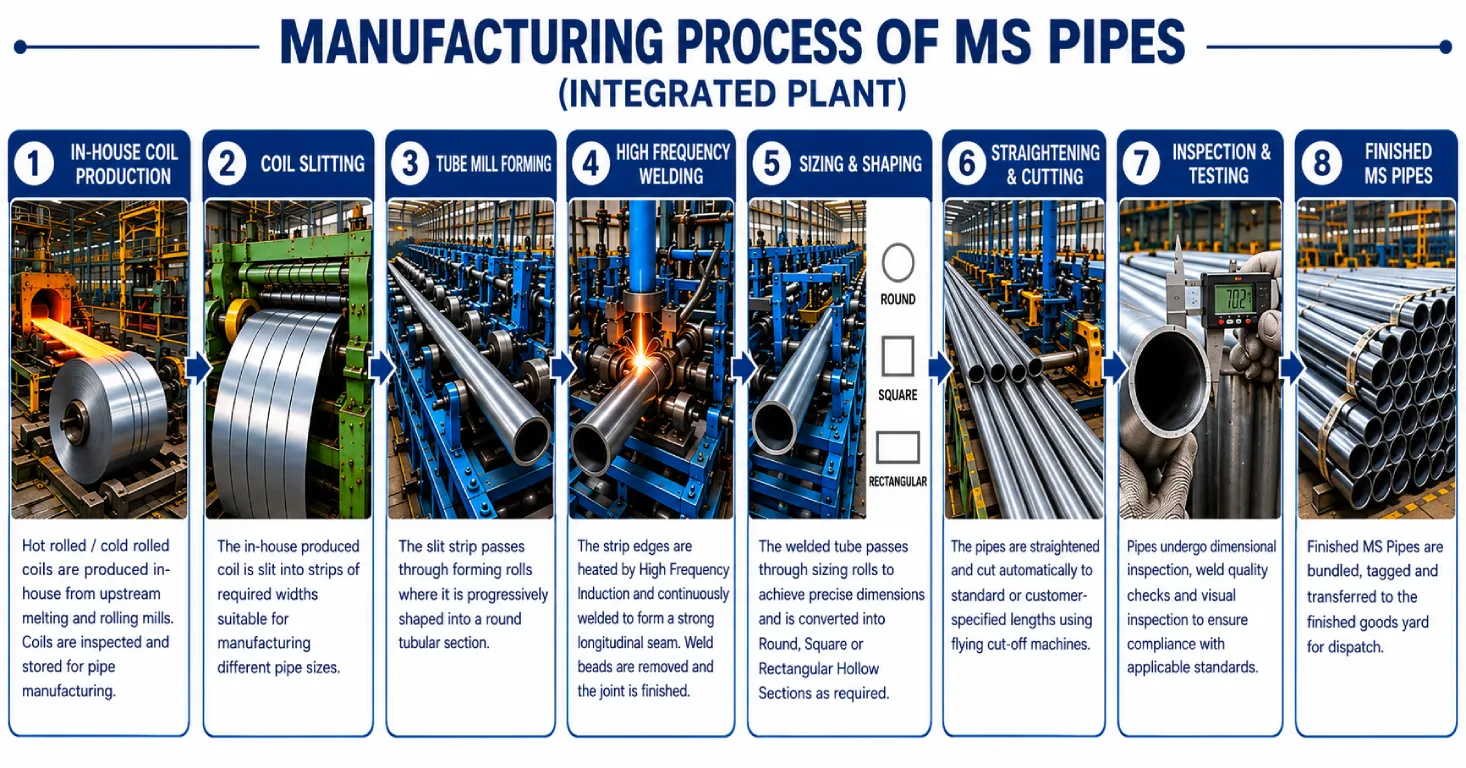
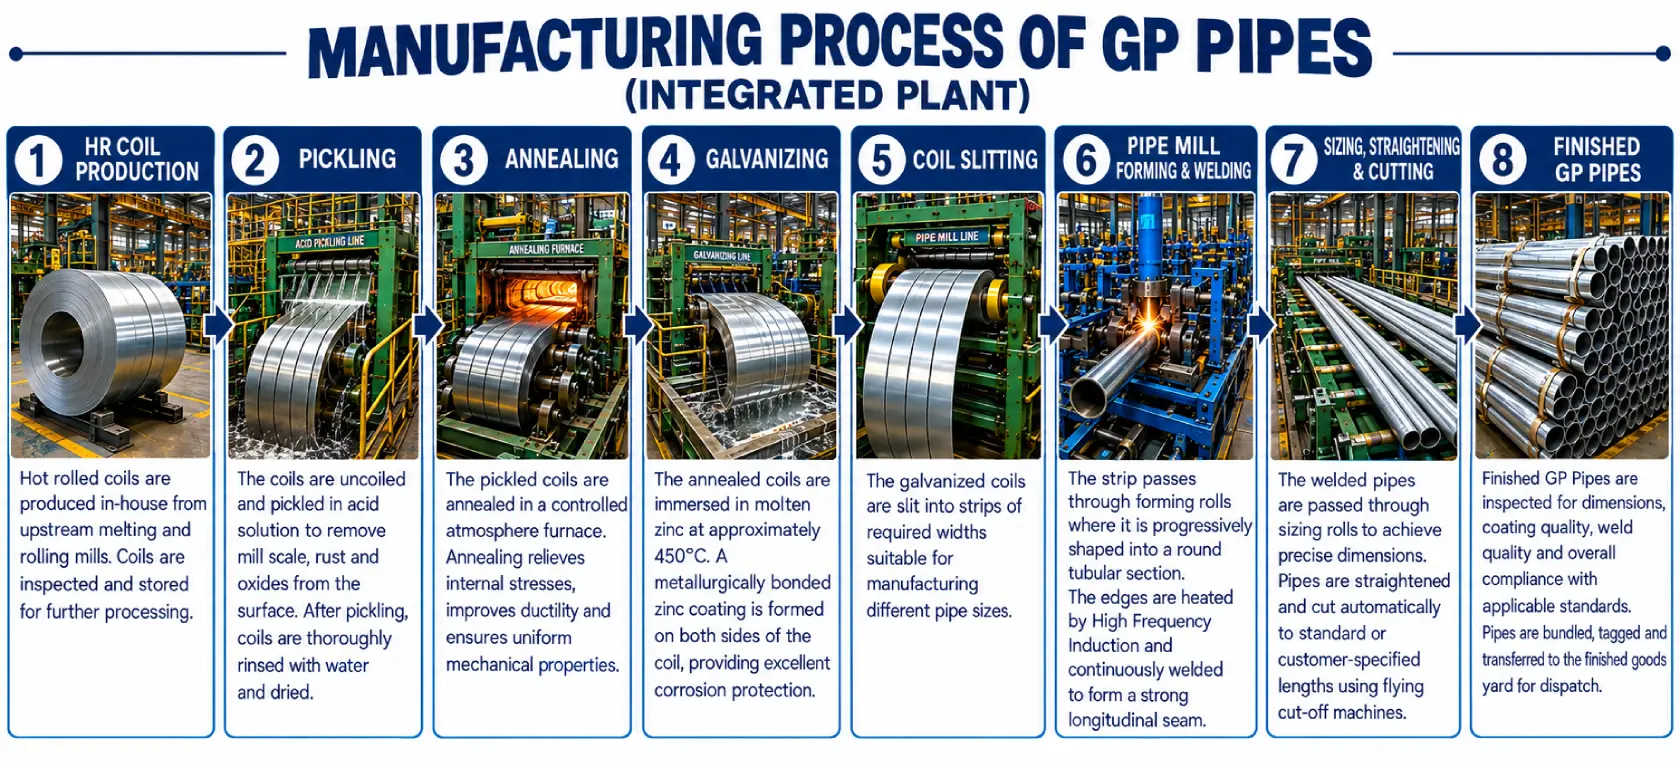
Our pipes and tubes portfolio includes HR (MS) Pipes, GP Pipes and CR Pipes. HR/MS Pipes are manufactured from hot-rolled steel, while GP Pipes are galvanized with zinc for corrosion resistance and CR Pipes are manufactured from cold-rolled steel.
Pipe dimensions:
Circular: 15 NB to 200 NB
Square: 15 × 15 mm to 150 × 150 mm
Rectangular: 40 × 20 mm to 200 × 100 mm
Thickness: 1 mm to 6 mm
Key features:
Multiple shapes and dimensions
Applications across construction, infrastructure and industrial sectors
Galvanized options for enhanced corrosion resistance
Precision and smooth-finish applications through CR Pipes
HR/MS Pipes are manufactured at Bellary Facility I, while GP Pipes and CR Pipes are manufactured at Bellary Facility II.
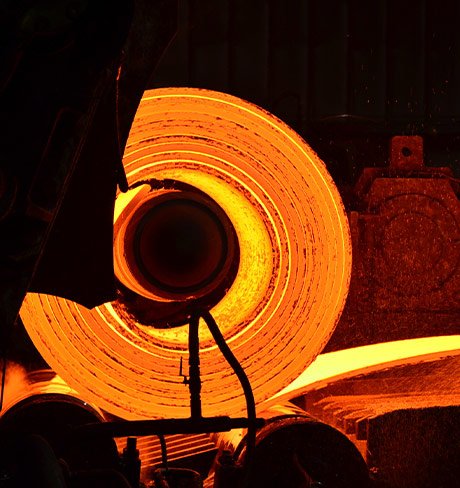
Hot Rolled
Hot Rolled Coil is a steel sheet product manufactured through controlled rolling and is used in downstream applications including pipes, tubes, automotive frames and industrial equipment.
Our HR Coil is manufactured at Bellary Facility I.
FY2026 installed capacity: 2,00,000 MTPA
FY2026 production: 1,70,384 MT
Capacity utilisation: 85.19%
Key features:
High ductility
Hot-rolled steel in coil form
Used for downstream manufacturing applications
Produced through our integrated Bellary manufacturing operations
Cold Rolled Coil
CR Coil is a cold-rolled steel product processed at lower temperatures and is used in applications requiring a smooth surface finish and dimensional precision.
Our CR Coil is manufactured at Bellary Facility II.
Key features:
Smooth surface finish
Suitable for precision applications
Used in automotive panels, appliances and other finished goods
Met Coke & Ferro Alloys
Our Chikkantapur Facility manufactures Met Coke and Ferro Alloys. Met Coke is a carbonized coal product used as a fuel and reducing agent in steelmaking, while our Ferro Alloys production includes Silico Manganese and Ferro Silicon, which are used in steelmaking to enhance properties such as strength and hardness.
FY2026 installed capacity:
Met Coke: 96,000 MTPA
Ferro Alloys: 37,100 MTPA
FY2026 production:
Met Coke: 90,776 MT
Ferro Alloys: 23,719 MT
High ductility
Hot-rolled steel in coil form
Used for downstream manufacturing applications
Produced through our integrated Bellary manufacturing operations
Quality & Finishing
Quality control is integrated across the manufacturing process. Molten steel undergoes spectrographic analysis, while finished products undergo relevant dimensional, mechanical, surface and quality inspections. Products that meet the required specifications are cut, packed, tagged for traceability and prepared for dispatch.
Our manufacturing process supports a portfolio of 10 product categories across intermediate, finished steel and industrial products.
1. Manufacturing Process of Sponge Iron (Direct Reduced Iron)